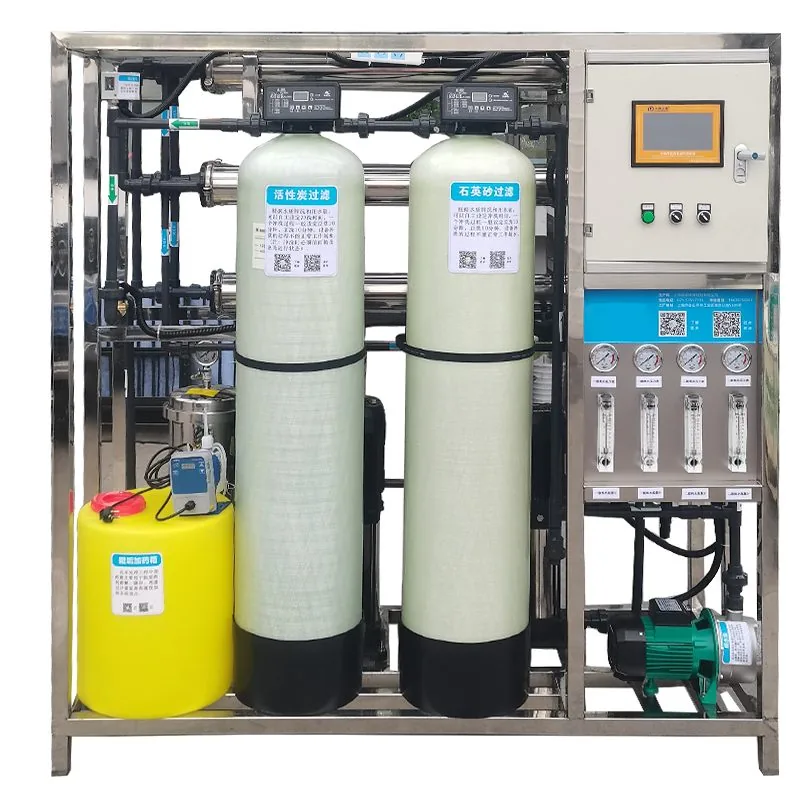
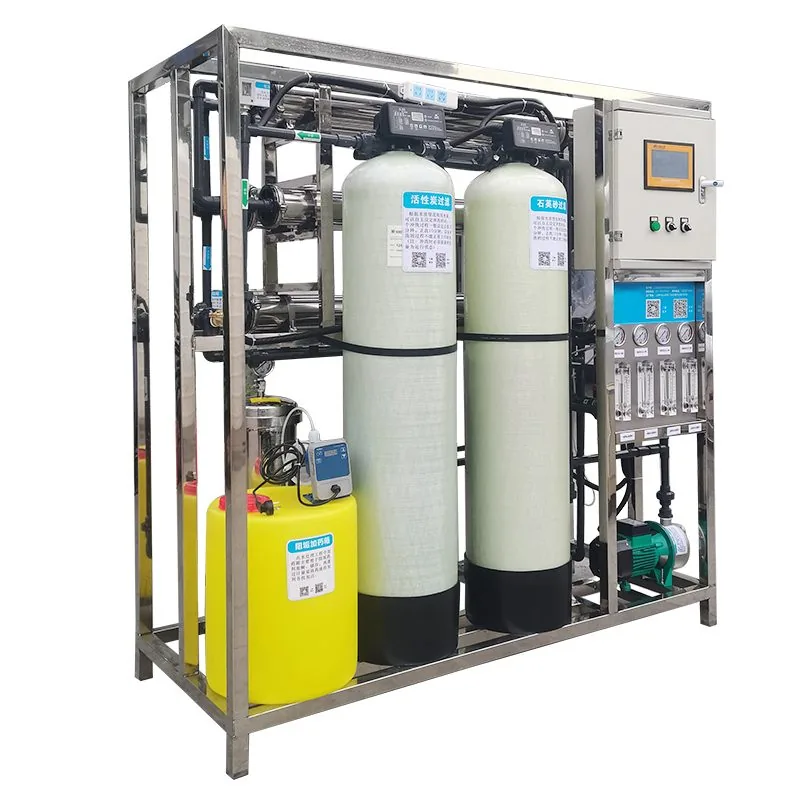
500 L/h dual-stage RO purified water system for laboratory, hospital pharmacy, and pilot-scale pharmaceutical production. Meets USP/EP/ChP pharmacopeia standards with conductivity below 1.1 uS/cm.
The PW-500 Laboratory Purified Water System is YohoAI's best-selling compact model designed for small-scale pharmaceutical production, hospital pharmacies, and R&D laboratories. Featuring a dual-stage reverse osmosis (RO) process with ozone and UV sterilization, the PW-500 reliably produces pharmacopeia-grade purified water at 500 L/h with conductivity below 1.1 uS/cm. cGMP-compliant construction with 316L stainless steel wetted parts ensures water purity throughout the production cycle.
Verified factory data - not marketing estimates
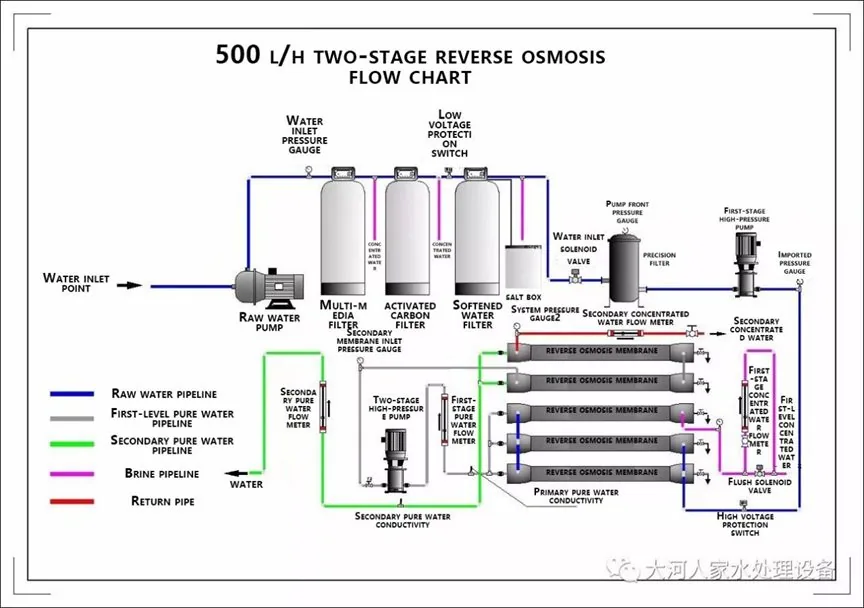
Two-pass reverse osmosis ensures product water meets USP, EP, and ChP pharmacopeia standards. Second-stage concentrate recycles to the raw water tank for 75%+ total recovery.
Conductivity below 1.1 uS/cm at 25 degC meets the strictest pharmaceutical water purity standards. Online conductivity meter provides real-time monitoring and alarm.
Ozone corona-discharge sterilization + 0.22 um PVDF sterilizing filter + 254 nm UV treatment eliminates bacteria, endotoxins, viruses, and prevents biofilm formation.
PLC + HMI touch screen displays flow rates, pressure, temperature, conductivity, ozone residual, and alarm history. Individual membrane sampling valves for on-site performance monitoring.
Fleck (USA) automatic control heads handle backwashing, forward flushing, and regeneration without manual intervention. Minimal operator maintenance required.
Full Installation Qualification (IQ), Operational Qualification (OQ), and Performance Qualification (PQ) documentation included. Material certificates 3.1/3.2 available for audit readiness.
Our team responds within 2 hours with CIF/CFR/FOB pricing and delivery timeline.
The PW-500 is rated at 500 L/h at 25 degC feed water temperature. For every 1 degC below 25 degC, output drops by approximately 2.1%, so sizing should account for your lowest winter water temperature. At 15 degC, expect roughly 420 L/h output. Capacity is also affected by feed water TDS, with lower TDS improving both flow rate and recovery.
The standard IQ/OQ package includes Installation Qualification protocols, Operational Qualification test records, Performance Qualification acceptance criteria, material certificates (3.1/3.2) for all wetted parts, P&ID diagrams, FAT/SAT protocols, and risk assessment documentation. IQ/OQ is included in the base price; extended PQ support and regulatory submission assistance are available for an additional fee.
Single-pass RO typically produces water at 5-50 uS/cm conductivity, which does not meet pharmacopeia standards. The PW-500's dual-stage RO achieves <1.1 uS/cm-roughly 5-10x purer than single-pass. Second-stage concentrate recycling also raises overall recovery from ~60% (single-pass) to 75%+, significantly reducing wastewater disposal costs.
Base PW-500 system pricing is quoted per project for the standard skid with ozone + UV sterilization and basic PLC control. Adding EDI for ultra-low conductivity (<0.1 uS/cm), online TOC analyzer, SCADA integration, or expanded IQ/OQ documentation packages raises the quoted price. Free installation, commissioning, and operator training are included.
The 5 um cartridge filter should be replaced every 3-6 months depending on feed water quality. RO membrane chemical cleaning is needed when operating pressure rises to 1.2 MPa (vs. 0.8 MPa baseline)-typically every 6-12 months under normal conditions. Membranes last 2-5 years with proper maintenance. All replacement intervals are documented in the operation manual provided with each system.
Every unit is built to order, so a firm price comes from your specification, not from a catalogue. Six points decide it: target output per hour, product type (powder, granules, pellets, oil, cream), package format and size, voltage and frequency, certification and documentation package, and delivery terms. Send those six points and you receive a written offer with price, lead time and scope of supply within 24 hours. No obligation, NDA on request. Use the six-point specification form.
Standard delivery ranges from 30-90 working days depending on the model and configuration. Pharmaceutical GMP configurations with validation documentation packages require additional 5-10 working days. Expedited manufacturing is available for urgent orders at a 15-25% premium.
All YohoAI machines carry CE certification and are designed to meet cGMP and ISO9001 standards. Additional certifications including FDA compliance and specific food-grade standards are available depending on the product line and configuration.
The PW-500 is a skid-mounted system designed for straightforward installation in laboratory or hospital pharmacy environments. Position the unit on a level floor with adequate drainage and access to municipal tap water (TDS below 500 ppm), a drain for concentrate discharge, and a 220V/380V power supply. Connect the feed water inlet, concentrate drain, and product water outlet per the P&ID drawing provided. Allow minimum 1 meter clearance on all sides for membrane housing access and cartridge replacement. YohoAI includes free on-site commissioning and operator training with every system.
Daily operation is fully automated via the PLC + HMI touch screen. The Fleck automatic control heads manage pre-treatment backwashing, forward flushing, and softener regeneration without operator intervention. Monitor the HMI daily for conductivity readings, flow rates, pressure trends, and alarm status. The 5 um cartridge filter requires replacement every 3-6 months depending on feed water turbidity. RO membrane chemical cleaning is needed when operating pressure rises to 1.2 MPa versus the 0.8 MPa baseline, typically every 6-12 months under normal conditions.
Preventive maintenance extends RO membrane life to 2-5 years and ensures consistent pharmacopeia-grade water quality. Weekly ozone sanitization cycles prevent biofilm formation in the product water path. The 0.22 um PVDF sterilizing filter should be replaced every 6-12 months based on integrity testing results. Keep a spare set of cartridge filters, UV lamp, and PVDF filter on hand to minimize downtime. All replacement intervals are documented in the operation manual, and YohoAI provides spare parts sourcing support for the lifetime of the system.
A hospital pharmacy in the Middle East operates the PW-500 as the sole purified water source for IV admixture preparation and reagent-grade laboratory work. The system runs continuously at approximately 400 L/h during peak demand hours, with the 316L stainless steel storage tank buffering supply during high-consumption periods. The ozone + UV triple-barrier sterilization has eliminated bacterial contamination events since installation, replacing a previous UV-only system that required weekly manual sanitization. At the hospital's feed water temperature of 22 degC, the PW-500 delivers 95% of rated capacity with 78% recovery, comfortably exceeding the 300 L/h peak demand for sterile compounding.
A nutraceutical contract manufacturer in North America uses the PW-500 to supply purified water for tablet press granulation, capsule filling equipment cleaning, and laboratory quality control. The 500 L/h capacity supports a two-shift operation with ample reserve for third-shift cleaning cycles. The conductivity alarm on the HMI triggers an automatic shutdown if water purity drops below 1.1 uS/cm, protecting product quality and preventing non-conforming batches from reaching packaging. The optional TOC analyzer upgrade, added 6 months after commissioning, now provides real-time organic contamination monitoring as required by the client's major retail customers for GMP certification renewal.
Step up to mid-scale pharmaceutical water production with SCADA-ready controls
Large-capacity multi-array RO for commercial pharma manufacturing
Complete cGMP documentation and validation package for pharmaceutical water systems