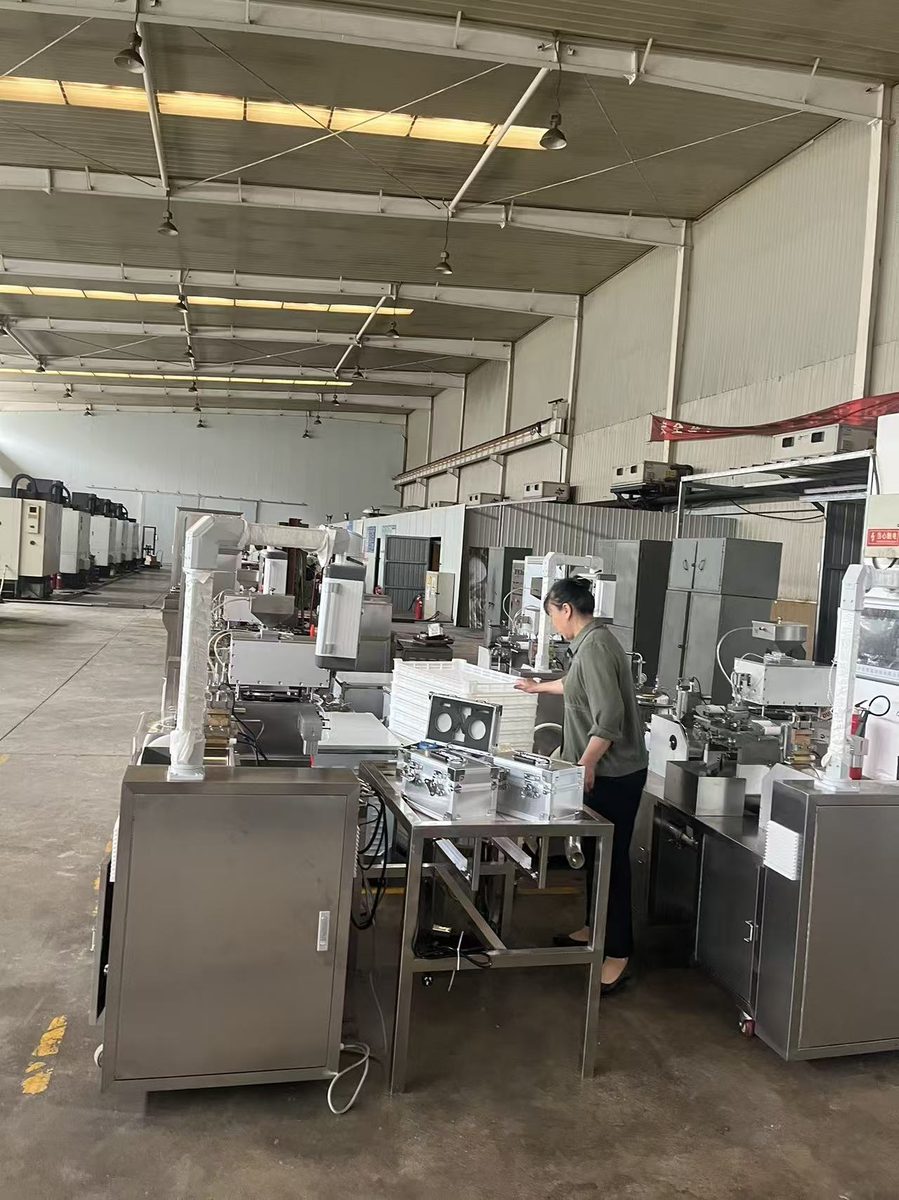
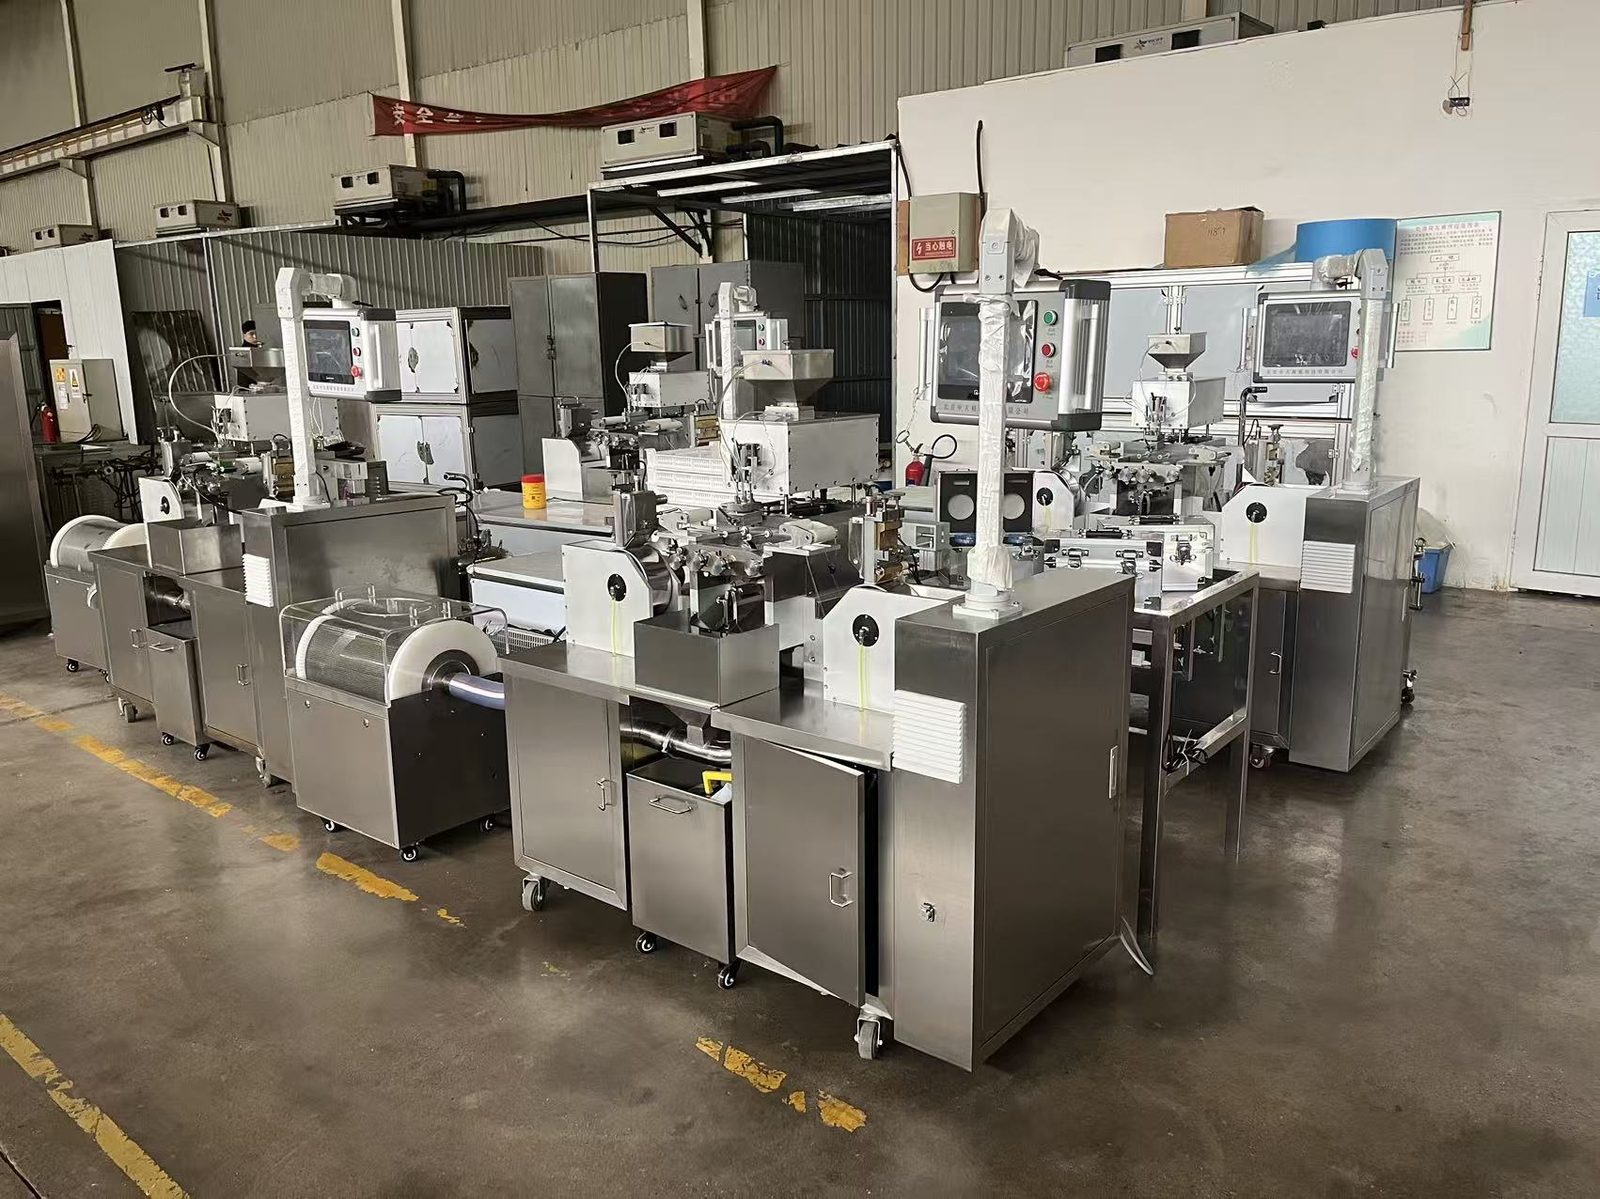
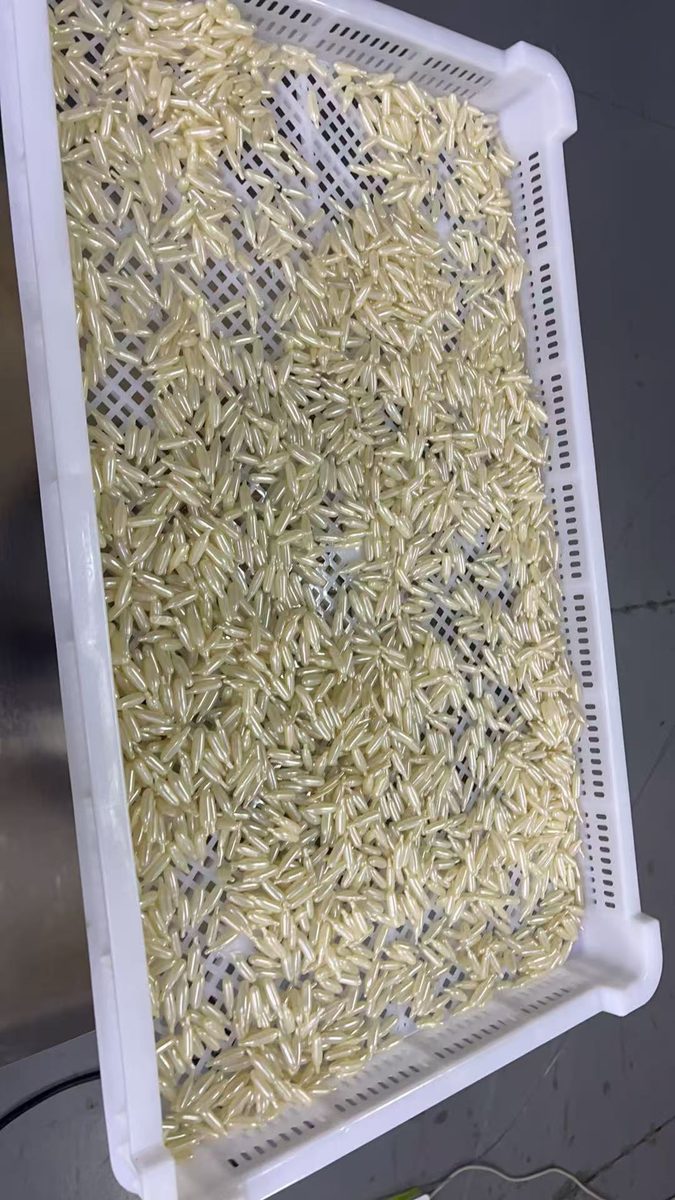
Turnkey high-speed encapsulation line delivering 228,000 capsules per hour for large pharmaceutical and nutraceutical factories.
The RG-8800 is a fully integrated high-speed softgel production line engineered for pharmaceutical factories requiring maximum throughput. Delivering 228,000 capsules per hour, it combines multi-die rotary encapsulation with integrated drying, inspection, and data management in one turnkey system.
Verified factory data - not marketing estimates
228,000 caps/hr via multi-station rotary die technology for mega-scale plants.
+/-1% servo pump with flow meter for consistent high-value dosing.
Integrated vision and weight check with automatic reject of off-spec capsules.
Integrated tumble drying zone tuned to 25C and 30% RH parameters.
10-inch HMI with recipe management, data logging, and factory network integration.
316L SS, Ra <=0.4 um, CIP-compatible, full validation documentation.
Our team responds within 2 hours with CIF/CFR/FOB pricing and delivery timeline.
The RG-8800 delivers 228,000 capsules per hour using multi-die rotary encapsulation technology. It is engineered for pharmaceutical factories and mega-scale nutraceutical plants that require maximum throughput with consistent quality across continuous 24/7 production shifts and large export volumes.
Yes. The RG-8800 is a turnkey high-speed line with integrated drying, in-line inspection, and automatic reject of off-spec capsules. It meets CE, cGMP, and ISO 9001 standards with full DQ/IQ/OQ/PQ documentation for FDA, EMA, and Health Canada submissions.
The RG-8800 uses precision servo pumps with flow meters to achieve +/-1% filling accuracy across oils, suspensions, pastes, and semi-solids. In-process weight control and automatic rejection of off-spec capsules ensure batch consistency required by pharmaceutical and nutraceutical quality systems.
The line integrates vision and weight inspection with automatic reject of off-spec capsules. Controlled drying at 25C and 30% relative humidity, plus 316L stainless steel contact parts with Ra <=0.4 um surface finish, preserves sealing integrity and appearance at full speed.
The RG-8800 processes gelatin, HPMC, and pullulan shells with fully adjustable temperature, humidity, and dosing parameters. Standard HPMC vegetarian capability supports halal and kosher formulations, enabling plant-based and clean-label supplement production at industrial scale.
The RG-8800 features a 10-inch HMI with recipe management, alarm logging, and production data export. It is MES-ready for factory network integration using Siemens or Mitsubishi PLC controllers, supporting traceability and batch record automation for regulated manufacturing.
Engineers provide on-site installation, commissioning, and operator training, plus a free Shanghai factory process trial. A 12-month warranty covers parts and labor, with lifetime technical support, remote diagnostics, and spare parts shipped within 48 hours to protect line uptime.
Pricing for the RG-8800 turnkey line is quoted on configuration, automation, and certification scope. Chinese high-speed systems typically offer 40 to 60 percent savings versus European brands while meeting the same CE, cGMP, and ISO 9001 compliance requirements for pharmaceutical factories.
The RG-8800 turnkey line demands extensive facility preparation before installation. A dedicated pharmaceutical-grade cleanroom with precise climate control at 22-26 deg C and 30-45% relative humidity is required, along with adequate structural support for the multi-die rotary line and auxiliary equipment. Three-phase power with industrial-grade switchgear, motor drives, and emergency stop circuits must be installed per the engineering drawings supplied by YohoAI. Compressed air, nitrogen (for oxygen-sensitive fills), and drainage connections should be routed before machine delivery. Installation, commissioning, and IQ/OQ validation typically require 2-3 weeks on-site with YohoAI engineers, included in the standard quotation.
Continuous 24/7 operation of the RG-8800 demands rigorous production monitoring and shift handover protocols. Operators must verify line status on the 10-inch HMI at every shift change, confirm no outstanding alarms exist, and check that the MES recipe loaded matches the current production order. The integrated vision and weight inspection system requires daily calibration verification using reference capsules to maintain reject rate within specification. Monitor drying zone parameters continuously at 25 deg C and 30% RH; deviations beyond +/-2 deg C or +/-5% RH must trigger an immediate process review before resuming production. All production data logged by the MES-ready system should be reviewed and countersigned per batch record requirements.
Preventive maintenance on a high-speed multi-die line must be planned during scheduled production stops to minimize throughput loss. Each production cycle should be followed by a cleaning and inspection window. Daily tasks: wipe down all 316L stainless steel surfaces, verify the reject station clears correctly, and confirm the drying tunnel airflow is unobstructed. Weekly actions: CIP cycle on all manifolds, inspection of multi-die sealing stations for wear, and calibration verification of the vision inspection system. Monthly maintenance covers replacement of all seals in the filling circuit, dimensional inspection of die rolls across all stations, and verification of the PLC control system's MES data interface integrity. Quarterly service should include full motor drive diagnostics, pneumatic system overhaul, and re-validation of the OQ/PQ protocols for regulatory compliance with FDA and EMA standards.